Temperature range of liquid ammonia: –77 °C to +130 °C
Specific Requirements Regarding Leak-Tightness and Operational Safety
At the same time, the medium places high demands on leak-tightness, material selection and operational safety. Ammonia is toxic, harmful to health in higher concentrations and can corrode certain materials. Safe, hermetically sealed pump systems are therefore required for its transfer – particularly at low temperatures and in applications involving changing states of matter.
Everything You Need to Know About Ammonia
Why is ammonia one of the most important natural refrigerants? This white paper provides technical background information, explains its areas of application and offers practical insights for planning and operation. Download the white paper
Production of Ammonia (Ammonia Synthesis)
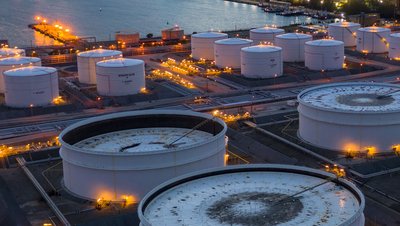
With an annual global production of around 180 million tonnes (as of 2021), ammonia is one of the most important basic chemicals in industry. It is produced from nitrogen and hydrogen, usually using the Haber-Bosch process.
HERMETIC Canned Motor Pumps are used in the synthesis process, amongst other things, to remove condensed ammonia and to transfer liquid ammonia to storage and holding tanks.
Application: Ammonia / Ammonia synthesis
- RequirementMedium: Ammonia (NH3)
Delivery rate: 15 m³/h
Pumping head: 45 m
Operating temperature: 40 °C
Advantages: Leak-free, durable - HERMETIC SolutionsPump: CNF 65-40-200
Motor: N34L-2
Pump type: Single-stage Canned Motor Pump
Ex protection: Yes
Speciality: High pump capacity, explosion protection
Cooling During Malt Separation
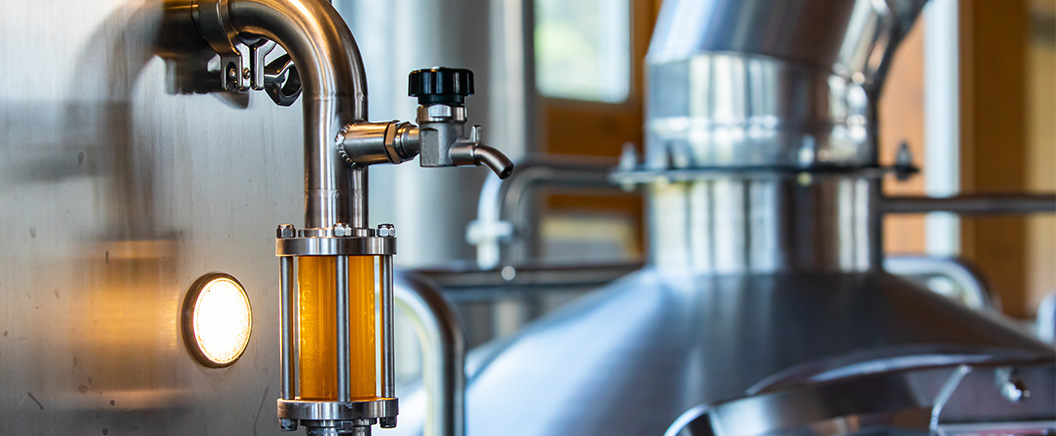
Ammonia (NH3) has established itself as the standard refrigerant in industrial refrigeration technology due to its excellent thermodynamic properties. In breweries, it is used, amongst other things, for cooling during malt separation. Furthermore, ammonia is used in central refrigeration systems in cold stores and deep-freeze facilities, abattoirs, chemical production plants and ice rinks.
Application: Ammonia
- RequirementMedium: Ammonia / R717
Delivery rate: 12 m³/h
Pumping head: 40 m
Operating temperature: –20 °C
Advantages: Leak-free, durable - HERMETIC SolutionsPump: CNF40-200
Motor: AGX4.5 (4.5 kW)
Pump type: Single-stage Canned Motor Pump
Ex protection: Yes
Speciality: High pump capacity
Can’t Find Your Application Here?
We’ll work with you to develop a suitable pump solution for your specific process requirements. Thanks to our many years’ experience in handling critical media, we can also produce bespoke designs and specialised solutions.
Get in Touch With Our Experts
Are you planning to use ammonia, or do you have any questions about conveying technology, design or possible applications? Please contact our team of experts. We’d be happy to advise you. Make an enquiry now